High-Power Fiber Laser Cutting Machines

Laser Cutting Thick Steel: Heavy Plate Solution

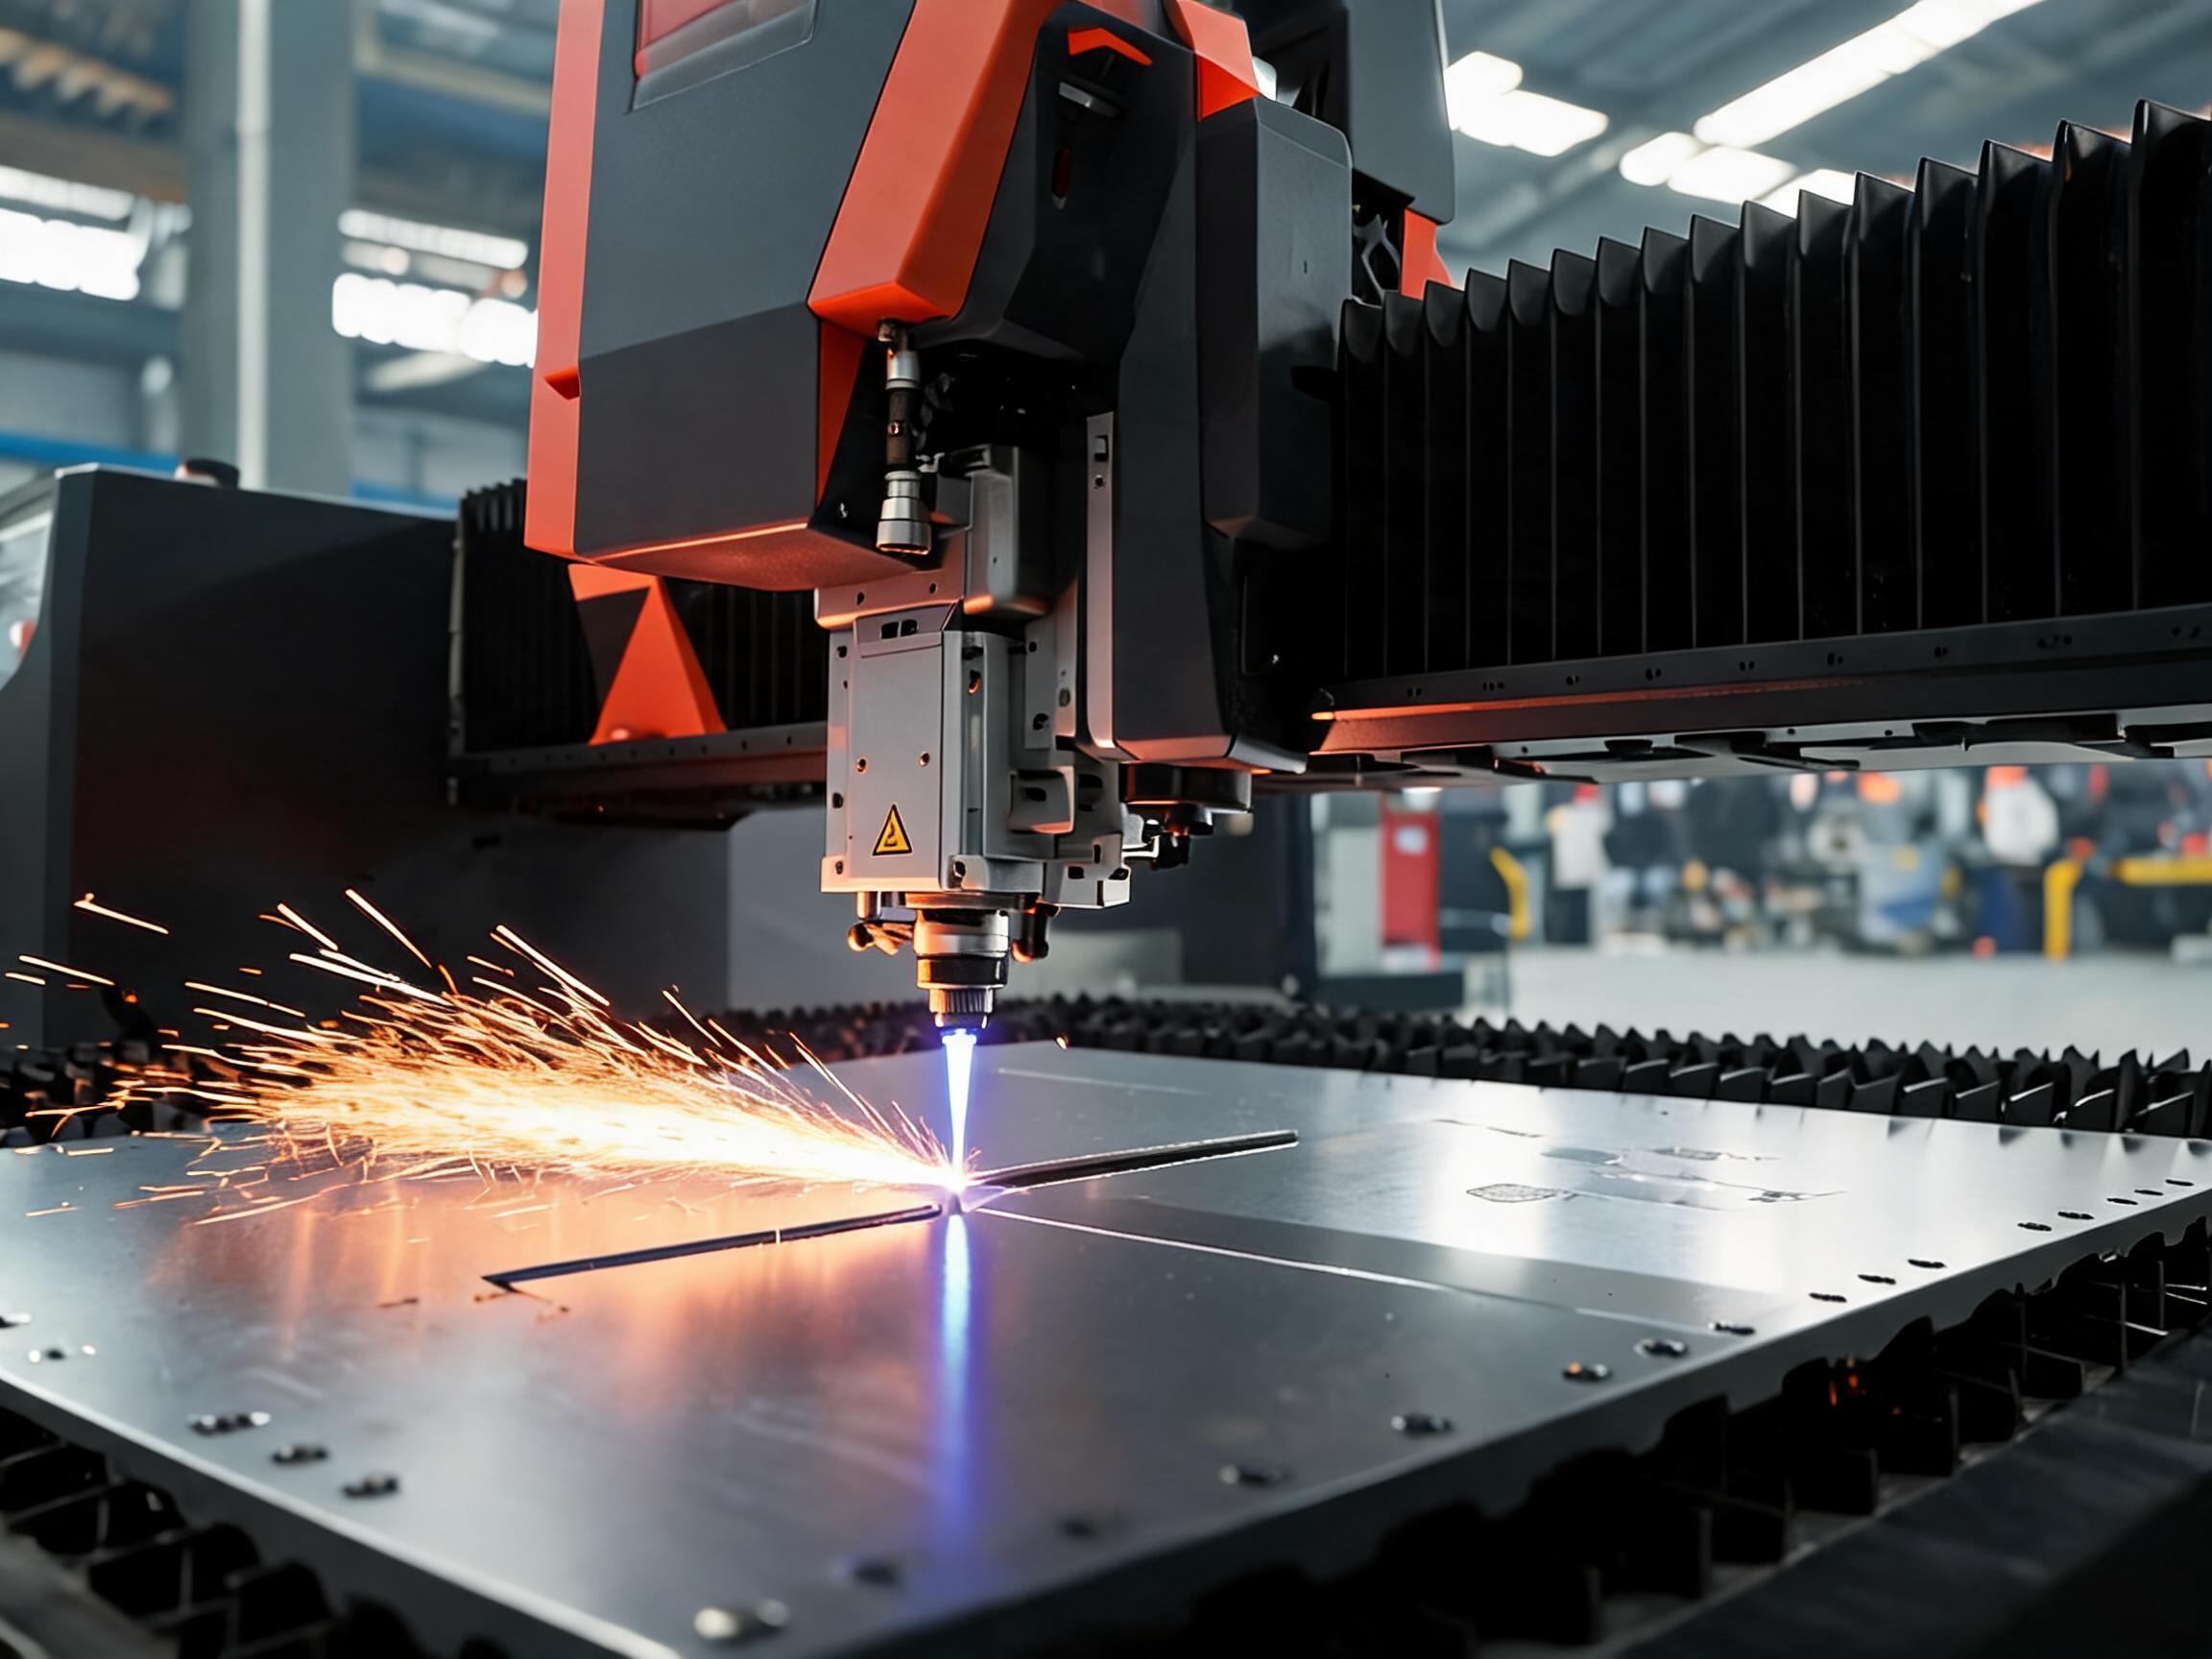
Match laser power to your real thick-plate mix: 8000W-30000W fiber platforms cut carbon steel from 25 mm to 70 mm with square edges instead of outsourced oxy-fuel and re-machining.

Request a quote
01Carbon steel to 25 mm
02Carbon steel to 35 mm
03Carbon steel to 40 mm

Thick plate is where the wrong cutting process quietly multiplies cost

Above roughly 20 mm, carbon steel punishes the wrong process. Flame and plasma cutting leave wide heat-affected zones and tapered edges, so every thick part carries a hidden machining allowance - and often a subcontract round trip. Buyers rarely see this cost on the quote; they see it in the grinding bay and in delivery delays.

What it costs you: machining allowance on every edge, extra handling between cutting and welding, outsourced lead time on plate above your current machine's limit, and rejected parts when the edge fails fit-up.

The process ladder: match power to your real thickness mix

Xinhong's high-power platforms cover the full thick-plate range with IPG, RAYCUS and GW fiber sources. Each step below is a specification limit from the product data sheet - your exact edge quality on your alloy is confirmed by a sample cut before order.

  1. 8000W: carbon steel to 25 mm, stainless to 16 mm - the entry step for serious thick-plate work.
  2. 12000W: carbon steel to 35 mm, stainless to 20 mm - heavy structural brackets and base plates.
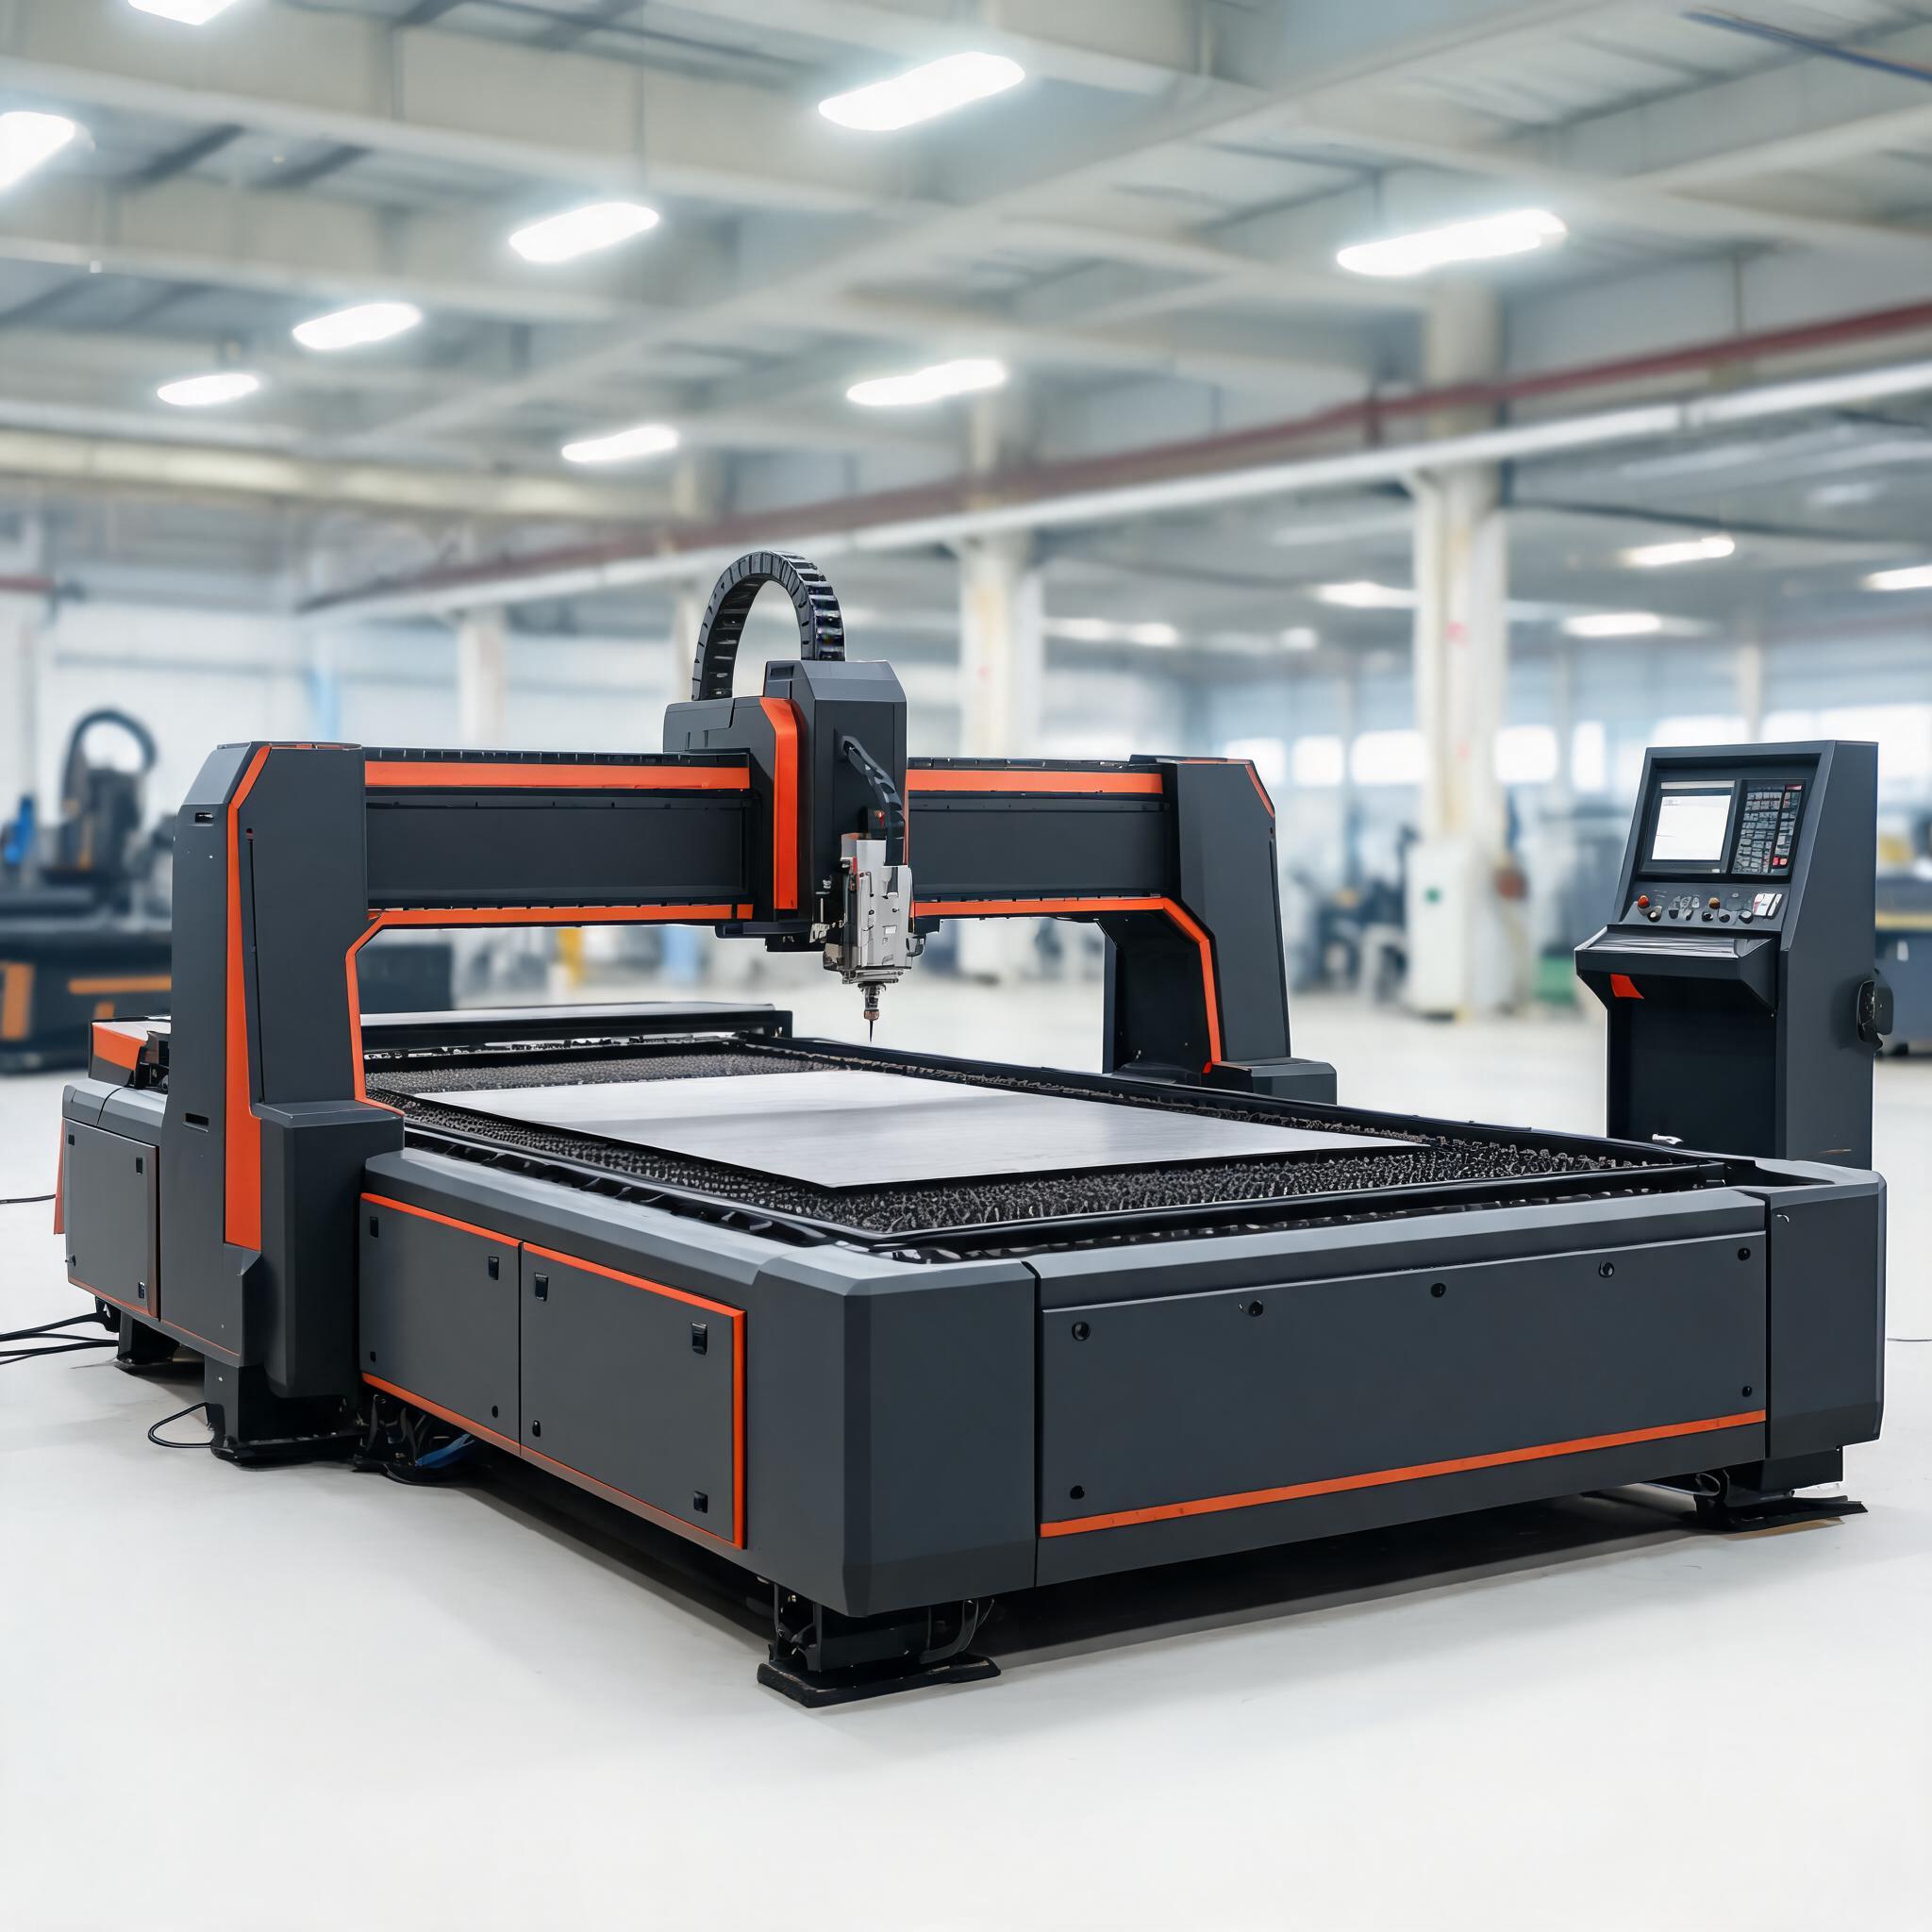
  3. 15000W: carbon steel to 40 mm, stainless to 25 mm, +/-0.05 mm positioning on a 2000 x 6000 mm bed.
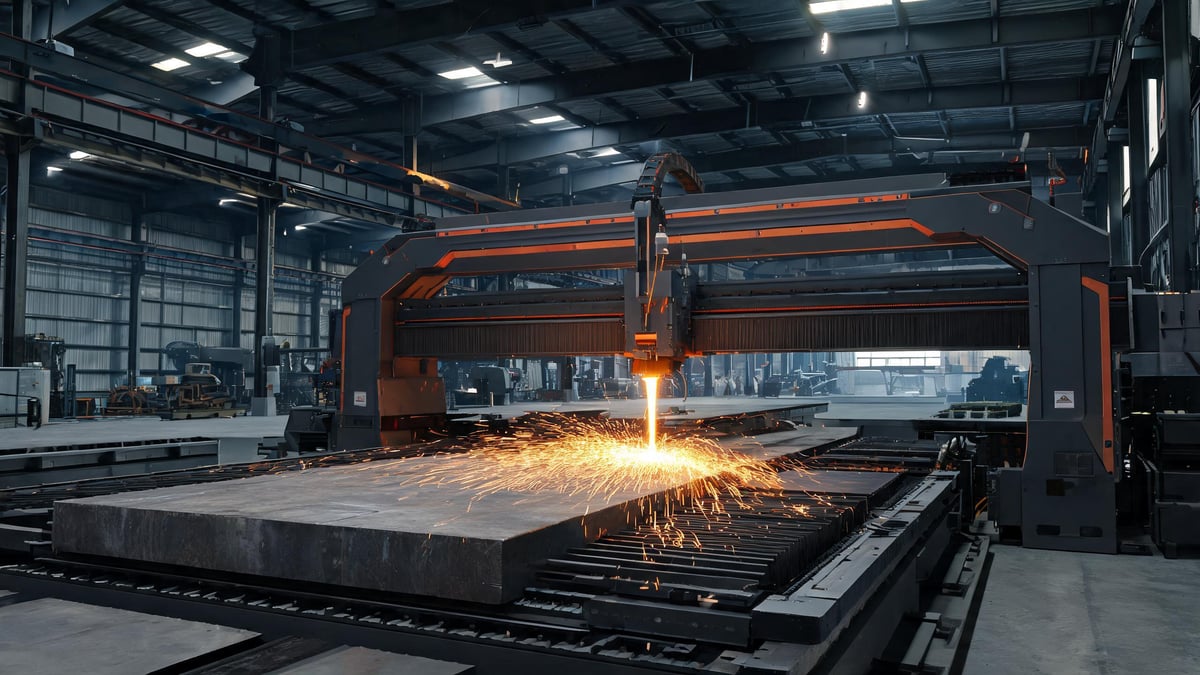
  4. 20000W marine platform: carbon steel to 50 mm, stainless to 30 mm - shipyard and offshore sections.
  5. 30000W flagship: carbon steel to 70 mm, stainless to 40 mm - the top of the current range.

What the buyer gets

One machine that covers your full thickness mix in-house: square edges that reduce or remove edge machining, no oxy-fuel subcontract round trips, and a power class chosen from your actual plate mix rather than from marketing. See the full machine range on our products page or send your thickness list through the inquiry form below - we respond with the recommended class and a sample-cut plan.

Buyer value: buy the lowest power class that covers your real thickness mix, keep thick parts on your own floor, and confirm edge quality on your own alloy before you sign.

Match your requirement to a machine

Recommended machine
8000W Fiber Laser Cutting Machine

8000W platform, 2000x6000 mm bed, stainless to 16 mm

View machine

Application case

Shipyard section fabricator: 25-50 mm frames cut in-house instead of outsourced oxy-fuel

Shipyard section fabricator: 25-50 mm frames cut in-house instead of outsourced oxy-fuel

Who: a shipyard section fabricator cutting hull frames and stiffeners. Machine: Xinhong 20000W marine engineering ultra-thick plate fiber laser cutting machine. Problem it solved: plate above 25 mm was sent out for oxy-fuel cutting, which delivered a wide heat-affected zone and a sizeable machining allowance on every edge. Before: outsourced oxy-fuel cutting meant transport, queue time and re-machining of bevels. Now: the marine platform cuts carbon steel to 50 mm (specification limit) in-house, so thick frames stay on the yard's own schedule. Where the numbers come from: the 20000W marine product specification (carbon steel to 50 mm, stainless to 30 mm) and the yard's own sample-cut report on their hull-grade plate; throughput is not claimed because it depends on plate handling and nesting.

Application based on customer feedback; individual results depend on materials and production conditions.
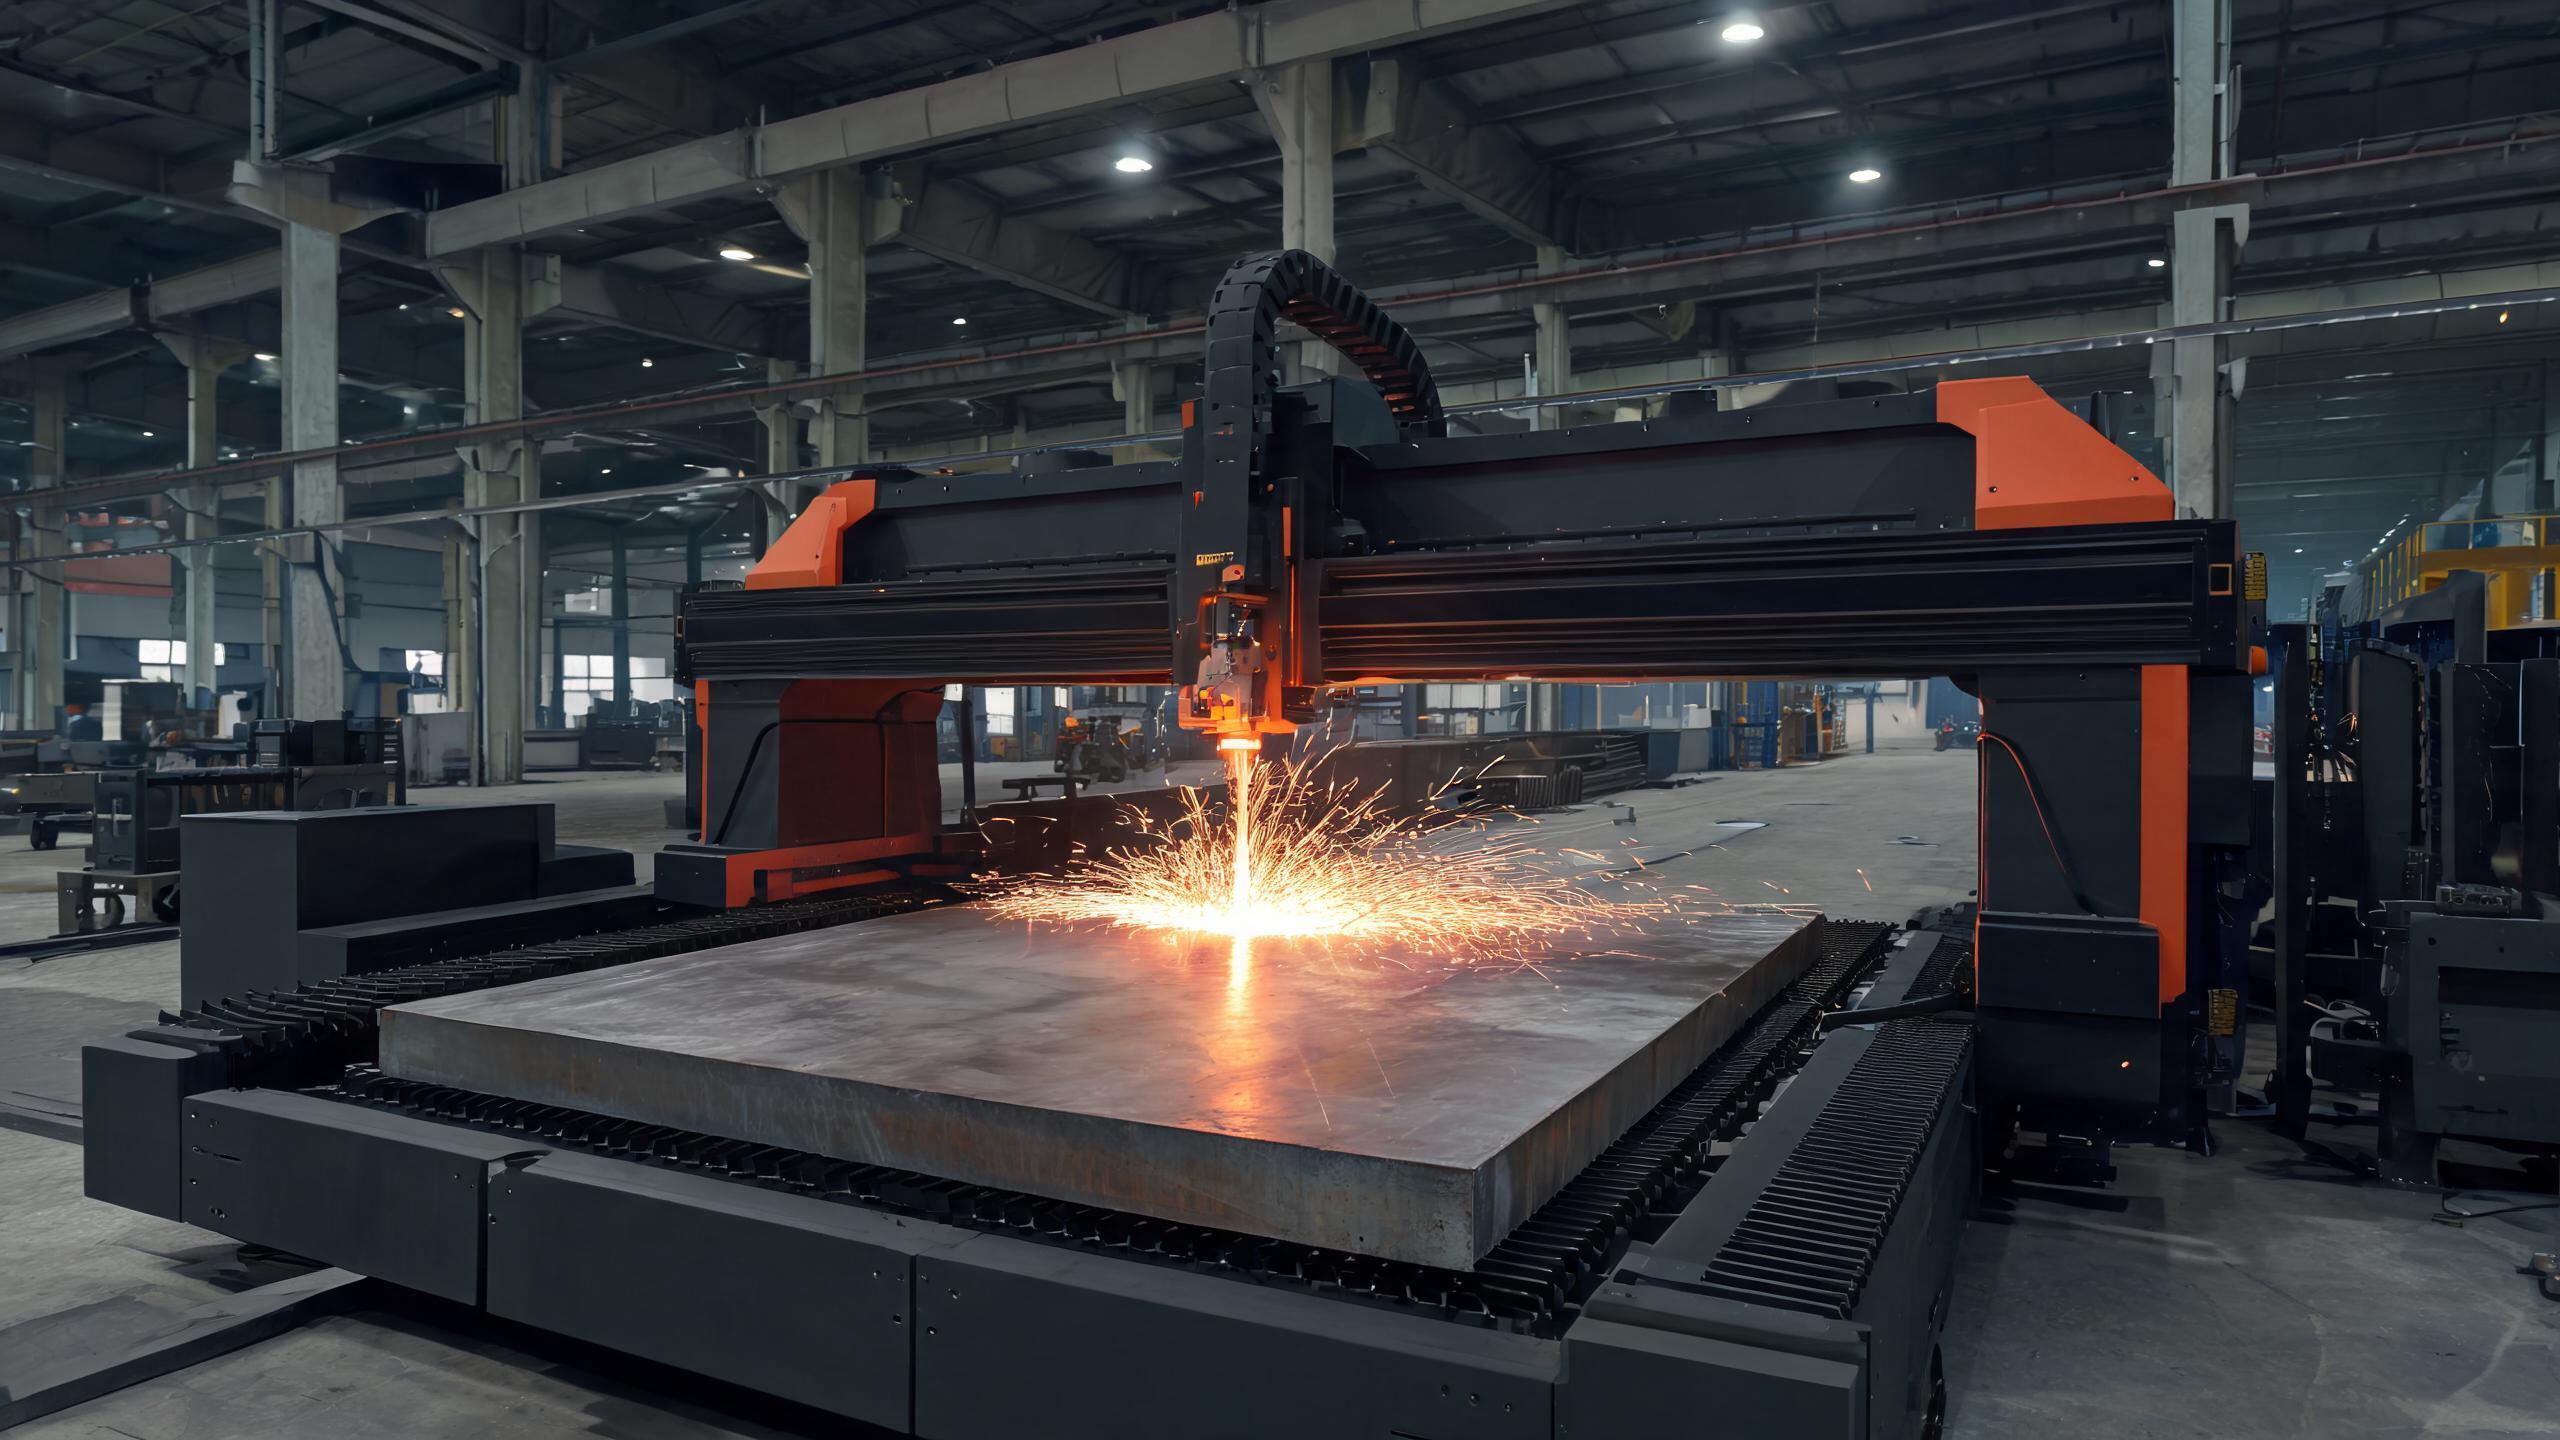

Structural steel fabricator: 20-35 mm brackets leave the grinding bench

Structural steel fabricator: 20-35 mm brackets leave the grinding bench

Who: a structural steel fabricator producing brackets and base plates for construction equipment. Machine: Xinhong 12000W fiber laser cutting machine. Problem it solved: 20-35 mm carbon steel parts were plasma cut, leaving a tapered bevel and dross that needed grinding before welding. Before: every bracket face was ground flat after cutting, and thick parts needed edge preparation by hand. Now: parts up to 35 mm carbon steel (specification limit) are cut square and go to the welding fixture as cut. Where the numbers come from: the 12000W product specification (carbon steel to 35 mm, stainless to 20 mm, 2000 x 6000 mm bed) and the fabricator's own sample-cut pieces compared side by side with their plasma parts; cycle time depends on nesting and material handling and must be measured on the buyer's own floor.

Application based on customer feedback; individual results depend on materials and production conditions.
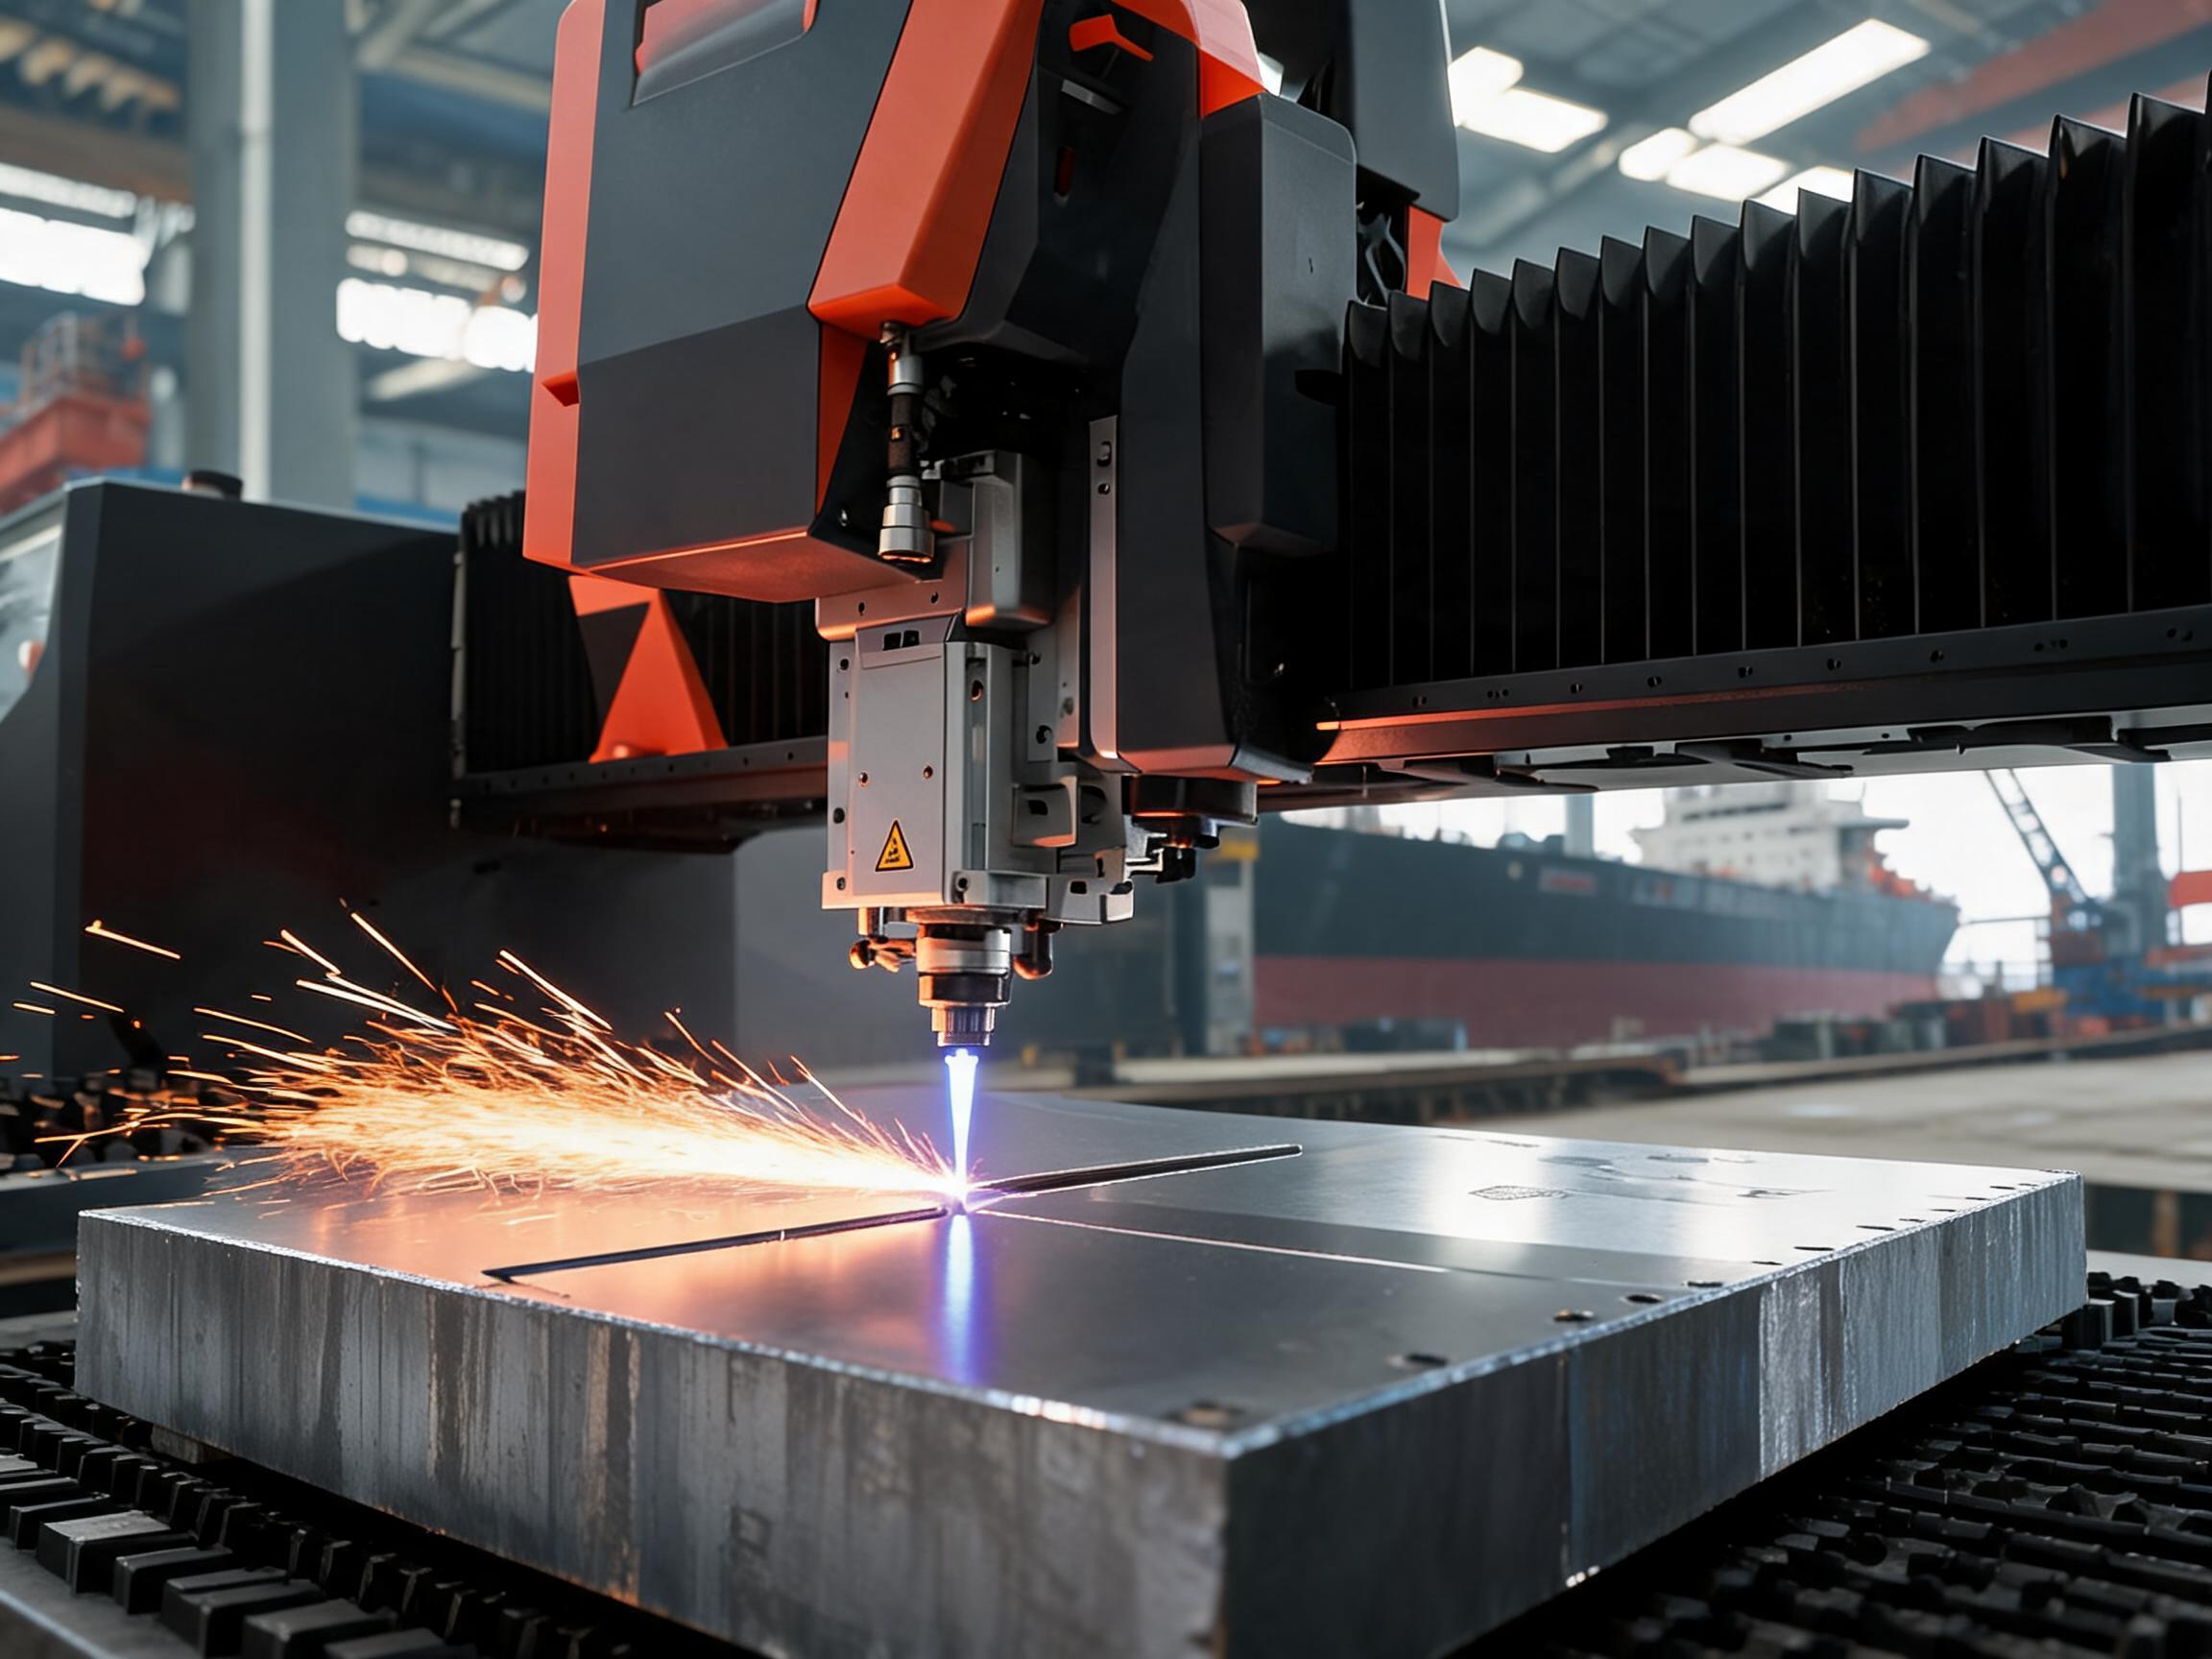
Heavy equipment OEM: 50-70 mm wear plate in one cutting pass

Who: a heavy equipment OEM cutting wear plates and cutting edges from thick plate. Machine: Xinhong 30000W fiber laser cutting machine. Problem it solved: 50-70 mm wear plate was flame cut and then milled on the edge before assembly, so every part crossed two departments. Before: flame-cut edges carried a wide heat-affected zone that machinists removed before hard-facing. Now: the 30000W platform cuts carbon steel to 70 mm (specification limit), so edge preparation is reduced to the buyer's own acceptance criteria. Where the numbers come from: the 30000W product specification (carbon steel to 70 mm, stainless to 40 mm) and the OEM's trial-cut report on their own wear-plate grade; cost per part depends on assist gas and nesting and must be quoted from a sample cut.

Application based on customer feedback; individual results depend on materials and production conditions.
Customer ratings

β€œUse case: 20-35 mm brackets and base plates for construction equipment, quoted through an RFQ with sample cuts. | Assessment: we compared the laser edges against our plasma parts before signing, and the square edge is what moved us - not the wattage. | Verified point: the 12000W specification lists carbon steel to 35 mm on a 2000 x 6000 mm bed, and the sample parts we kept match the drawing. | Source: buyer RFQ email thread and retained sample-cut parts, 2025.”
Production plannerStructural steel fabricator, EU (anonymised)
β€œUse case: hull frames in 25-50 mm plate, evaluated during a commissioning visit. | Assessment: our old route sent everything above 25 mm out for oxy-fuel; bringing it in-house changed our scheduling more than any cutting-speed figure. | Verified point: the 20000W marine specification lists carbon steel to 50 mm, confirmed on our own plate during the commissioning cuts. | Source: commissioning visit record and machine acceptance checklist, 2025.”
Workshop managerShipbuilding supplier, EU (anonymised)

Certifications & compliance

ISO 9001:2015

ISO 9001:2015

Quality management system certified across R&D, production and after-sales service of fiber laser cutting equipment.

CE Marking

Xinhong machines are CE marked for European markets per company records. Request the applicable Declaration of Conformity with your quotation.

Company strength

The factory behind your thick-plate line

Founded 2005Shandong Xinhong CNC Technology Co., Ltd - two decades of fiber laser equipment manufacturing.
100-300 employeesProduction, engineering and after-sales teams at the Shandong Province base.
Power range 500W-30000WA 48-model portfolio; the thick-plate ladder above sits at its top end.
Laser sourcesIPG (USA), RAYCUS and GW - source matched to power class.
Control componentsSchneider Electric electrical components fitted as standard.
Export marketsEurope and global markets with CE-compliant export configurations.

Related reading

Buyer FAQ

How thick can these machines cut carbon steel?+

Specification limits by platform: 8000W cuts carbon steel to 25 mm, 12000W to 35 mm, 15000W to 40 mm, the 20000W marine platform to 50 mm, and 30000W to 70 mm. Actual results on your alloy and edge-quality target are confirmed by a sample cut.

Do I still need edge machining after laser cutting thick plate?+

The edge face is square and the heat-affected zone is far narrower than flame or plasma cutting. Whether it removes your machining allowance entirely depends on your downstream tolerance - send your part drawings for a sample cut and we return the measured edge.

Which power class fits a mixed 10-50 mm workload?+

Yes. The thickness ladder above maps power to carbon steel and stainless limits. Send your thickness range, alloy grades and monthly volume and we recommend the lowest power class that covers your full mix - over-buying power is the most common way buyers inflate cost.

What should a thick-plate cutting inquiry include?+

Thickness range, alloy grades, plate sizes, edge quality expectation and monthly tonnage. With these we run a sample cut on matching plate and quote power class, bed size and assist-gas setup together.

Request a quotation for this solution

Send your requirement details below - our engineers will confirm the right machine configuration in your quotation.

Laser Cutting Thick Steel: Heavy Plate Solution

β–Έ QUOTE REQUEST

FORM Β· REV.1
Product Inquiry
Laser Cutting Thick Steel: Heavy Plate Solution