
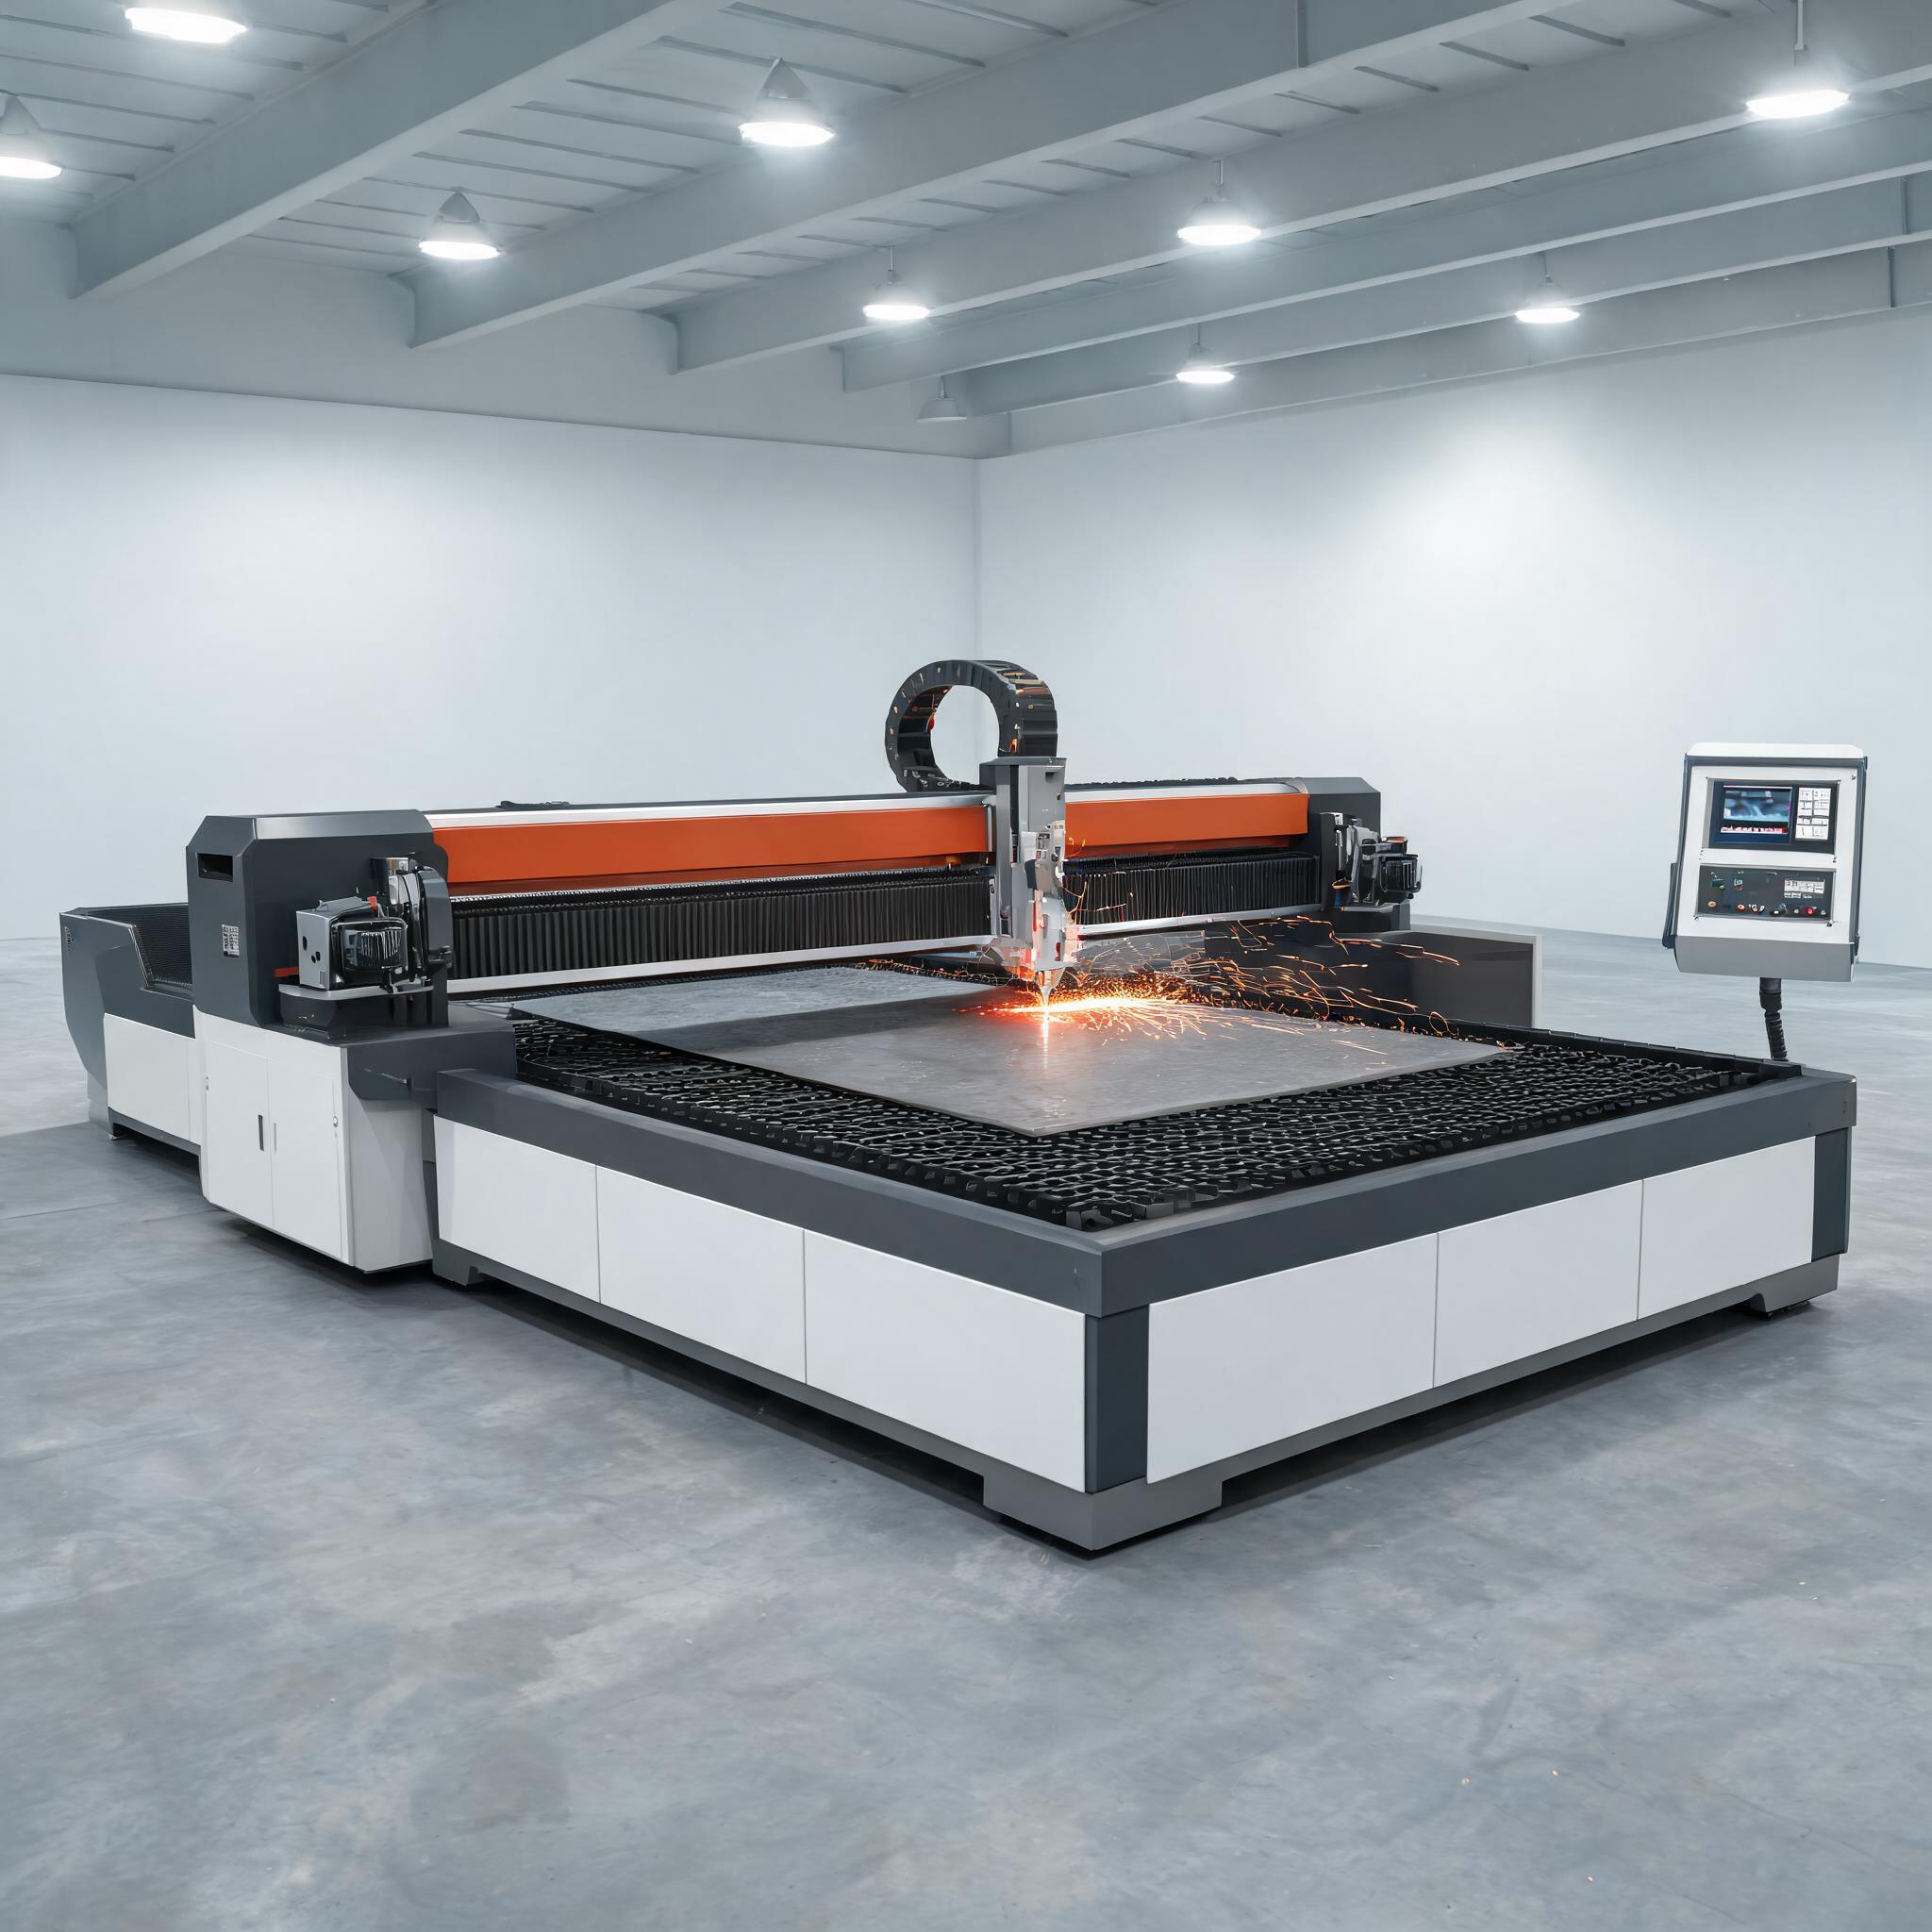
6000W fiber laser cutting machine cutting carbon steel plate with oxygen assist

High-Power Fiber Laser Cutting Machines

Carbon Steel Laser Cutting Solution

Oxygen-assisted fiber laser cutting for carbon steel: 3000W-30000W platforms matched to your real 6-20 mm gauge mix, with sample cuts and written thickness tables before you order.

Request a quote

Buying a carbon steel laser cutter: the oxygen cutting decision

The pain most carbon steel fabricators arrive with

Carbon steel buyers rarely ask about wattage first. They arrive after one of three failures: an oxy-fuel bench that cannot hold edge quality on 8-16 mm S355, a plasma subcontractor whose bevel and heat-affected zone force grinding before every weld, or a machine bought too big for a gauge mix that rarely exceeds 12 mm. Each failure costs in the same currencies - rework hours, subcontract queues, and capital tied up in the wrong power class.

What it does to the purchasing decision

Because edge condition and pierce behaviour on carbon steel depend on oxygen pressure and power together, buyers who order on wattage alone routinely discover the mismatch only after installation. The result is a second round of tooling changes, edge-quality disputes and delays that a correctly specified machine would have avoided.

Our solution: power matched to your real gauge mix

Xinhong builds fiber laser platforms from 3000W to 30000W that cut carbon steel with oxygen assist from 12 mm up to 70 mm, with +/-0.05 mm positioning accuracy across the range. The matching work is done against your actual thickness histogram and grade list - not against a brochure table - and confirmed with sample cuts on your own material before you sign.

How the technology solves it

  • IPG, RAYCUS and GW laser sources paired per model with cutting heads tuned for oxygen-assisted carbon steel.
  • Schneider Electric control components and CypCut control software for repeatable pierce and cut parameters.
  • Servo-driven beds on the 2000x4000 mm and 2000x6000 mm platforms for heavy plate handling.
  • Optional auxiliary gas mixing system for shops that switch between oxygen, nitrogen and air workloads.

What you get as a buyer

A machine sized to the plate you actually cut, an agreed edge condition documented from sample cuts, and a quotation that states the gas strategy and thickness table behind it - instead of a wattage number you have to defend internally.

Match your requirement to a machine

Recommended machine
3000W Fiber Laser Cutting Machine

3000W cuts CS to 12 mm, +/-0.05 mm, 1500x3000mm bed

View machine

Application case

Structural steel fabricator: 8-16 mm S355 brackets cut in-house on 6000W

Who: a structural steel fabricator in Northern Europe, about 25 staff, cutting S355 brackets and connection plates for construction customers. Machine: Xinhong 6000W fiber laser cutting machine, 2000x4000mm bed. Problem it solved: a mixed 8-16 mm carbon steel workload had outgrown an ageing oxy-fuel bench, where slow piercing and wide kerfs forced heavy edge rework before welding. Before: oxy-fuel edges required grinding and re-marking, and thin jobs were subcontracted out. Now: 8-16 mm S355 cut in-house with oxygen assist on the 6000W platform, edges going to welding after light deburring. Where the numbers come from: the 6000W product specification (carbon steel to 20 mm, +/-0.05 mm repeatability, 50000+ hour tube life) plus the buyer's own sample-cut report on their 10 mm and 16 mm brackets; throughput comparisons depend on the buyer's nesting and handling and must be re-measured on their floor.

Application based on customer feedback; individual results depend on materials and production conditions.

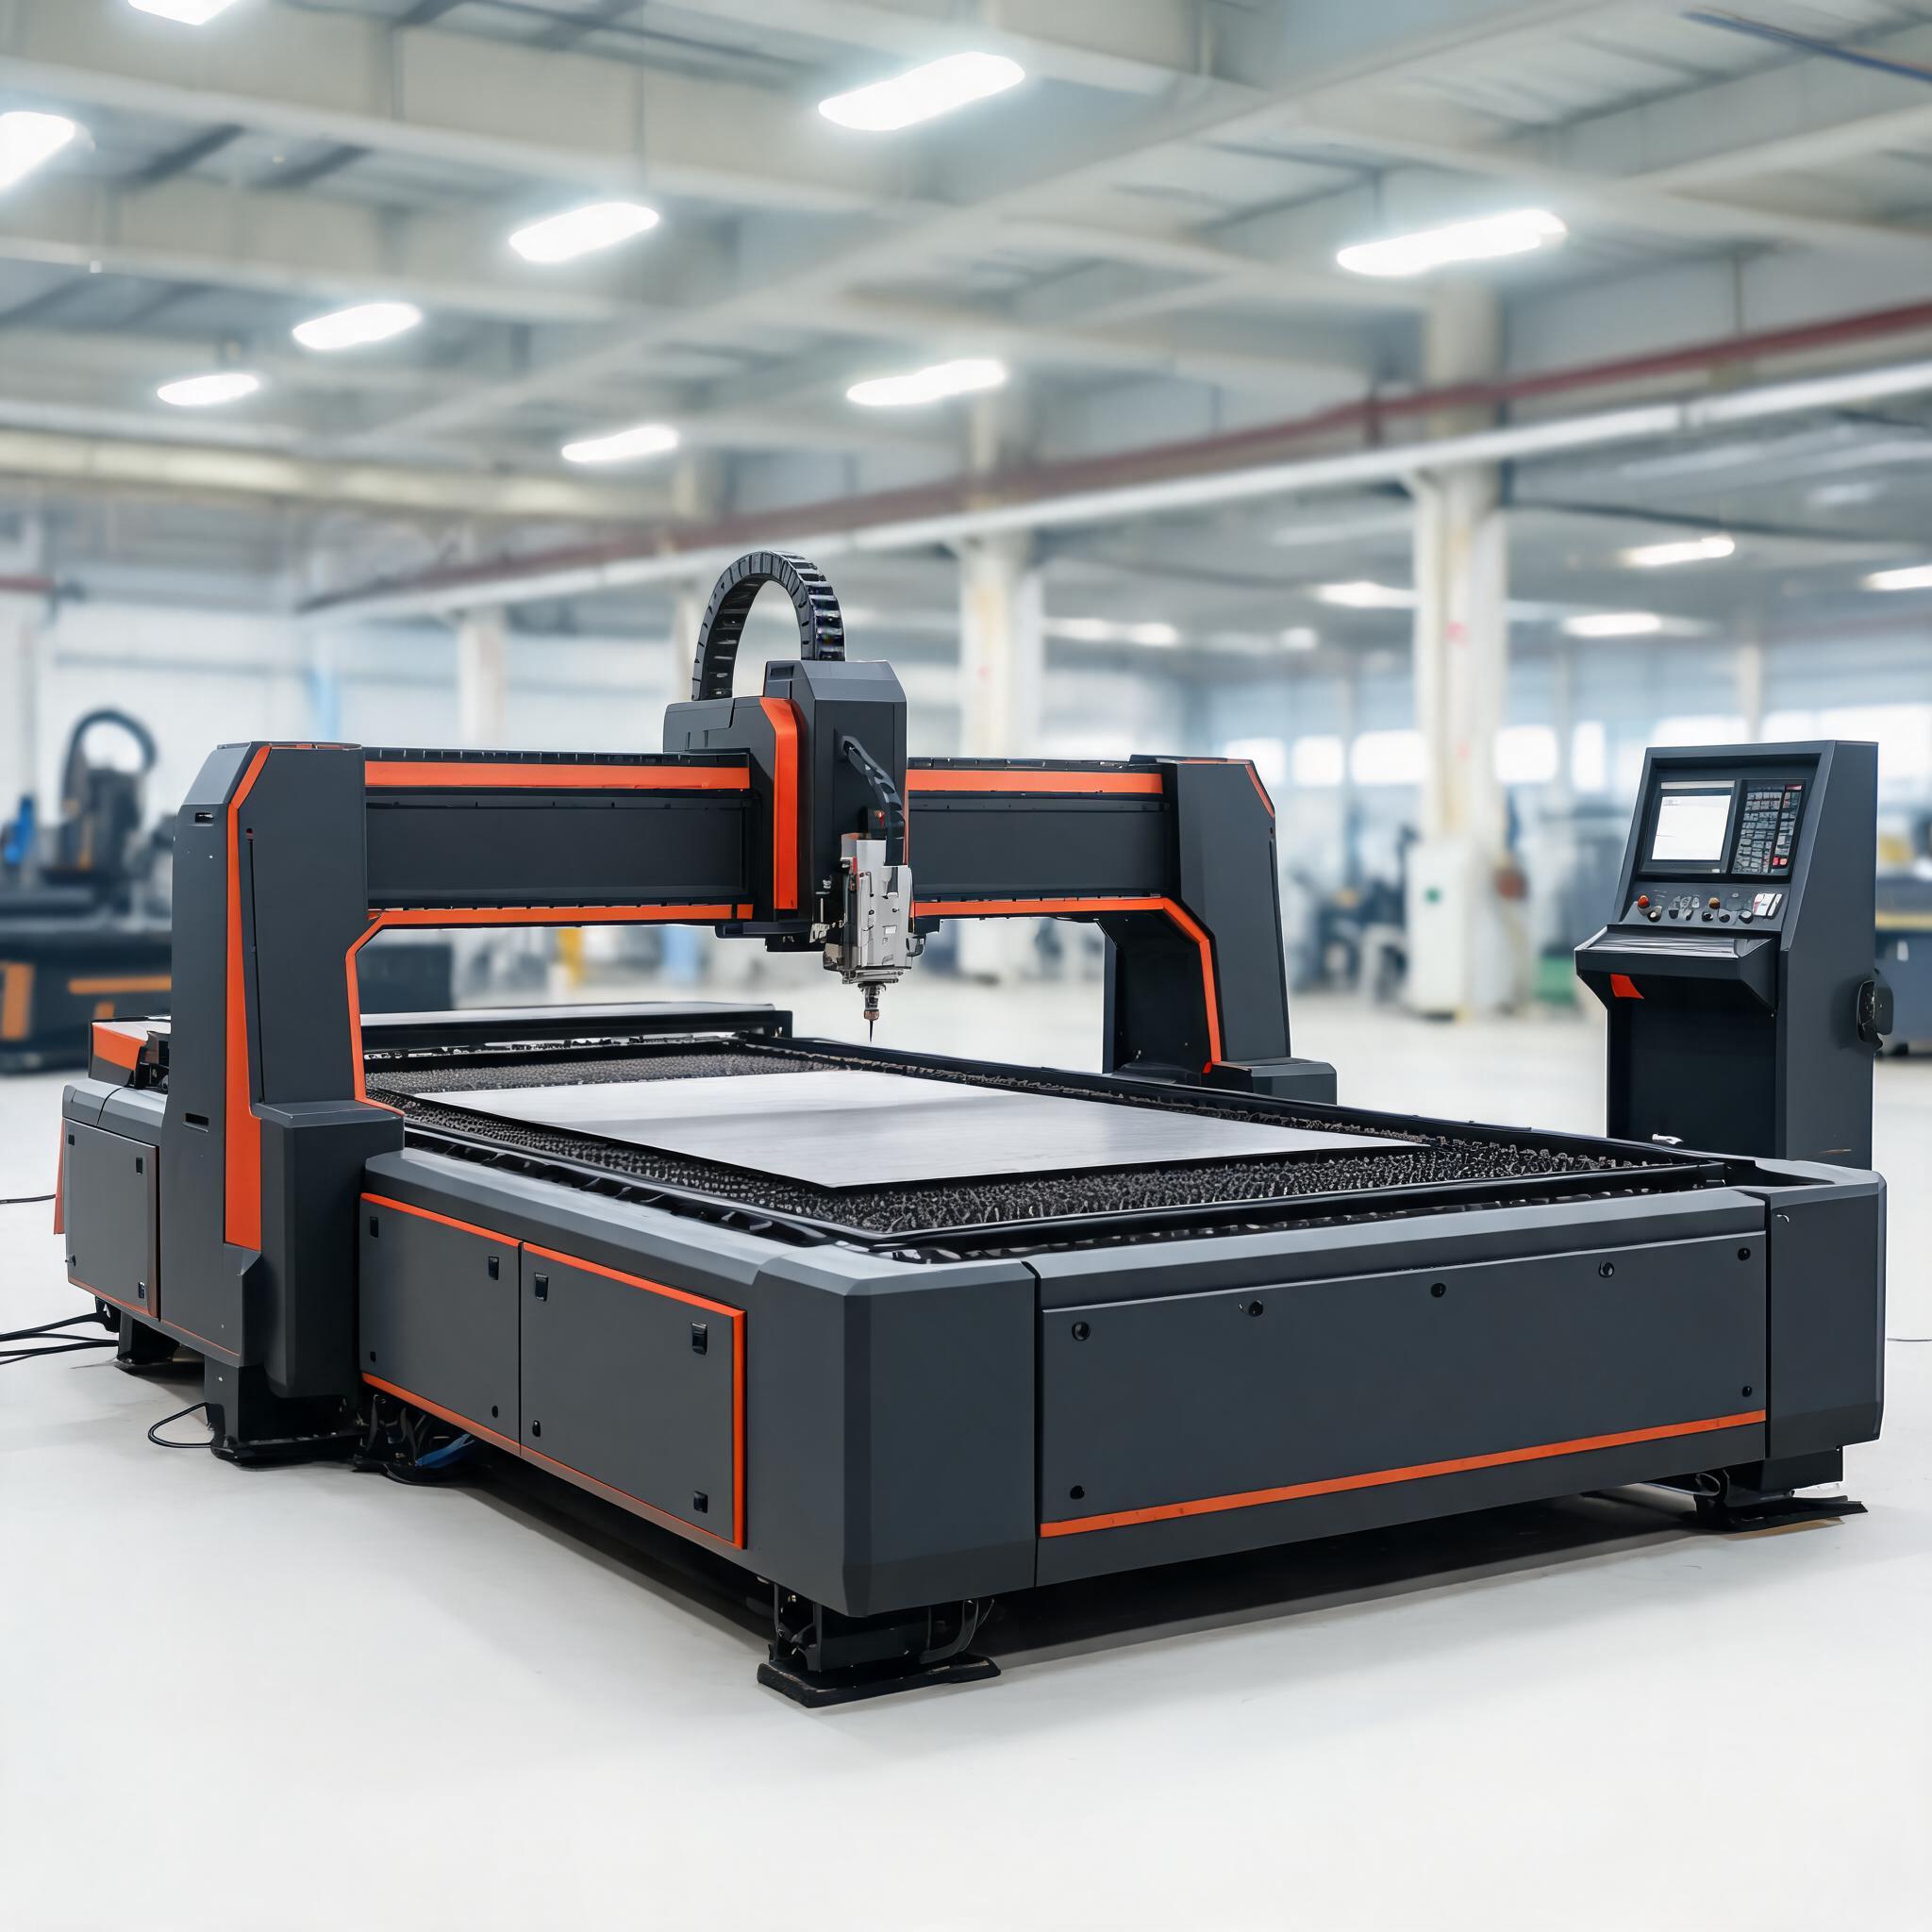
Agricultural implement maker: 15-20 mm brackets move off plasma subcontracting

Who: an agricultural implement manufacturer in Central Europe cutting wear and mounting plates for tillage equipment. Machine: Xinhong 8000W fiber laser cutting machine, 2000x6000mm bed. Problem it solved: 15-20 mm carbon steel brackets were going out to a plasma subcontractor, whose bevel and heat-affected zone needed extra grinding before welding. Before: outsourced plasma cutting with 3-5 days queue and hand-dressing of every edge. Now: 15-20 mm carbon steel cut in-house with oxygen assist on the 8000W platform, edges weld-ready after deburring only. Where the numbers come from: the 8000W product specification (carbon steel to 25 mm, +/-0.05 mm) and the buyer's own sample-cut report on their 15 mm and 20 mm brackets; cycle-time and cost comparisons must be established with a trial cut on the buyer's own material.

Application based on customer feedback; individual results depend on materials and production conditions.
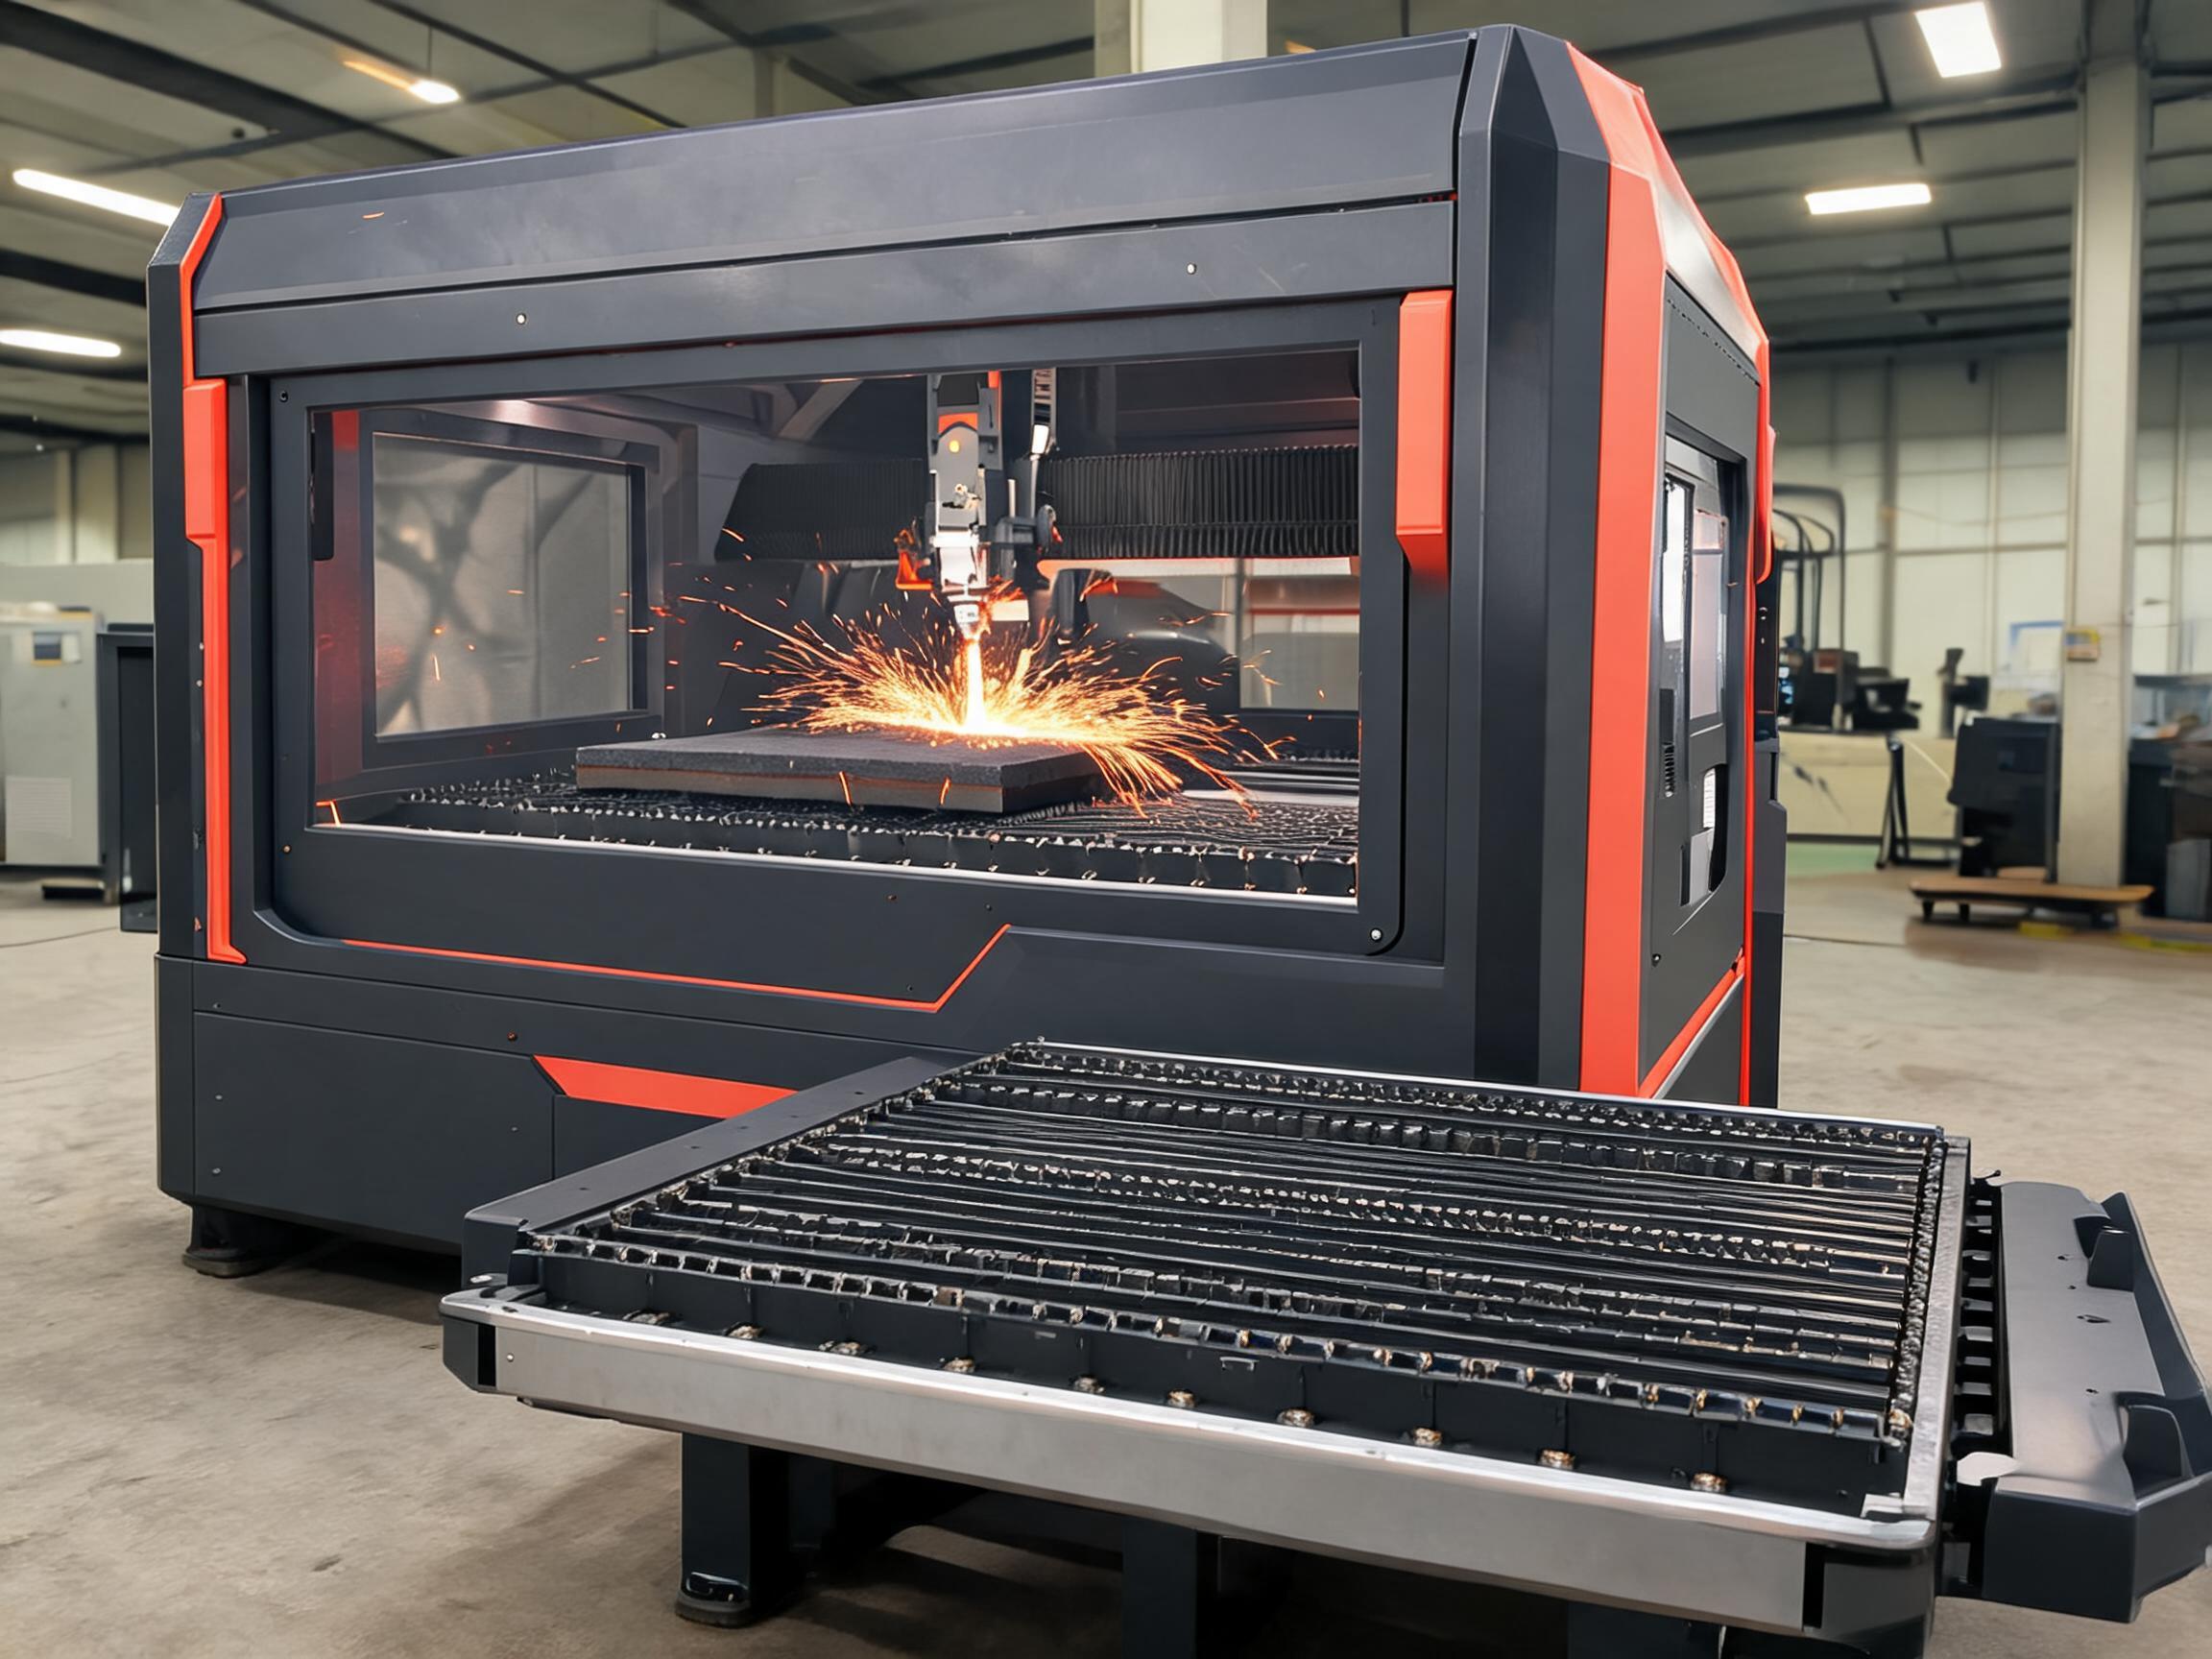
Who: a sheet metal job shop in Western Europe running mixed-gauge brackets, mostly 6-12 mm carbon steel. Machine: Xinhong 3000W fiber laser cutting machine, 1500x3000mm bed. Problem it solved: the shop could not justify a high-power machine for a workload that rarely exceeded 12 mm, but needed repeatable pierce quality on 10-12 mm plate. Before: 10-12 mm jobs delayed behind a single shared machine and often sent outside. Now: carbon steel to 12 mm cut on the 3000W platform with oxygen assist and +/-0.05 mm accuracy. Where the numbers come from: the 3000W product specification (carbon steel to 12 mm, +/-0.05 mm, 50000+ hour tube life) and the shop's own trial cuts on 10 mm and 12 mm plate; cost per part depends on oxygen price and nesting and must be confirmed with a quotation trial.

Application based on customer feedback; individual results depend on materials and production conditions.

Customer ratings

β€œUse case: S355 bracket and connection plate production for construction customers, 8-16 mm, sourced through a European agent. | Assessment: we asked for the oxygen cutting parameters in writing before we signed, and the sample edges on our own 10 mm and 16 mm plates were what closed the deal, not the wattage table. | Verified point: the specification lists +/-0.05 mm repeatability on the 2000x4000 mm bed, and our measured parts came back inside that band. | Source: buyer RFQ email thread and Xinhong sample-cut report, 2025.”
Production managerStructural steel fabricator, Northern Europe (anonymised)
β€œUse case: 15-20 mm bracket cutting brought in-house from a plasma subcontractor, purchased directly after a factory visit. | Assessment: we specified the machine against our bracket histogram rather than a peak job, and that conversation prevented us from overbuying power we would never use. | Verified point: carbon steel to 25 mm as listed for the 8000W platform, checked against our 20 mm wear-plate brackets in the acceptance cut. | Source: internal machine acceptance checklist, 2025.”
Plant engineerAgricultural implement manufacturer, Central Europe (anonymised)

Certifications & compliance

ISO 9001:2015

ISO 9001:2015

Quality management system certified across R&D, production and after-sales service of fiber laser cutting equipment.

CE Marking

Xinhong machines are CE marked for European markets per company records. Request the applicable Declaration of Conformity with your quotation.

Company strength

Who builds your carbon steel cutting machine

Founded 2005
Shandong Xinhong CNC Technology Co., Ltd has manufactured fiber laser equipment for two decades.
Factory scale
100-300 employees spanning machining, assembly, quality and service in Shandong Province, China.
R&D capability
Deep expertise in cutting thickness and cutting speed; core technologies developed with IPG (USA), RAYCUS and GW laser sources.
Production capacity
Annual revenue 10-50M USD supporting a 48-model portfolio from 500W to 30000W.
Component partners
Schneider Electric electrical control components fitted as standard.
Export markets
Europe and global markets, with CE-compliant export configurations.

Related reading

Buyer FAQ

Oxygen or nitrogen for carbon steel cutting?+

Oxygen assist is the standard, lowest-cost choice for 3-25 mm carbon steel and produces the familiar dark oxidised edge. Nitrogen gives a brighter edge on thin carbon steel but consumes far more gas. Your quotation should state which gas strategy was used for the sample cuts of your real gauges.

Which power class cuts which carbon steel thickness?+

Per current specifications: 3000W cuts carbon steel to 12 mm, 6000W to 20 mm, 8000W to 25 mm, 12000W to 35 mm, 15000W to 40 mm, 20000W to 50 mm and 30000W to 70 mm. Match power to your thickest recurring job, not your rarest one, and confirm with a sample cut.

Will oxygen-assisted edges need rework before welding?+

Oxygen-assisted cutting leaves an oxidised edge; the amount of dross and the rework needed depend on the gauge, gas pressure and pierce settings. Our acceptance practice is to cut your own bracket profiles before you order so edge condition is agreed in advance, not assumed.

What should I include in a carbon steel cutting machine inquiry?+

Include your carbon steel thickness mix, typical grades (for example S235, S355, wear plate), monthly tonnage, bed-size needs and target edge condition. We will confirm the power class, oxygen setup and bed size in the quotation.

Request a quotation for this solution

Send your requirement details below - our engineers will confirm the right machine configuration in your quotation.

Carbon Steel Laser Cutting Solution

β–Έ QUOTE REQUEST

FORM Β· REV.1
Product Inquiry
Carbon Steel Laser Cutting Solution